Tolerances & Quality
How CNC Machining Tolerances Affect Cost and Lead Time
Why blanket tight tolerances add setup, tooling, inspection, and scrap risk — and how to separate general tolerances from critical features.
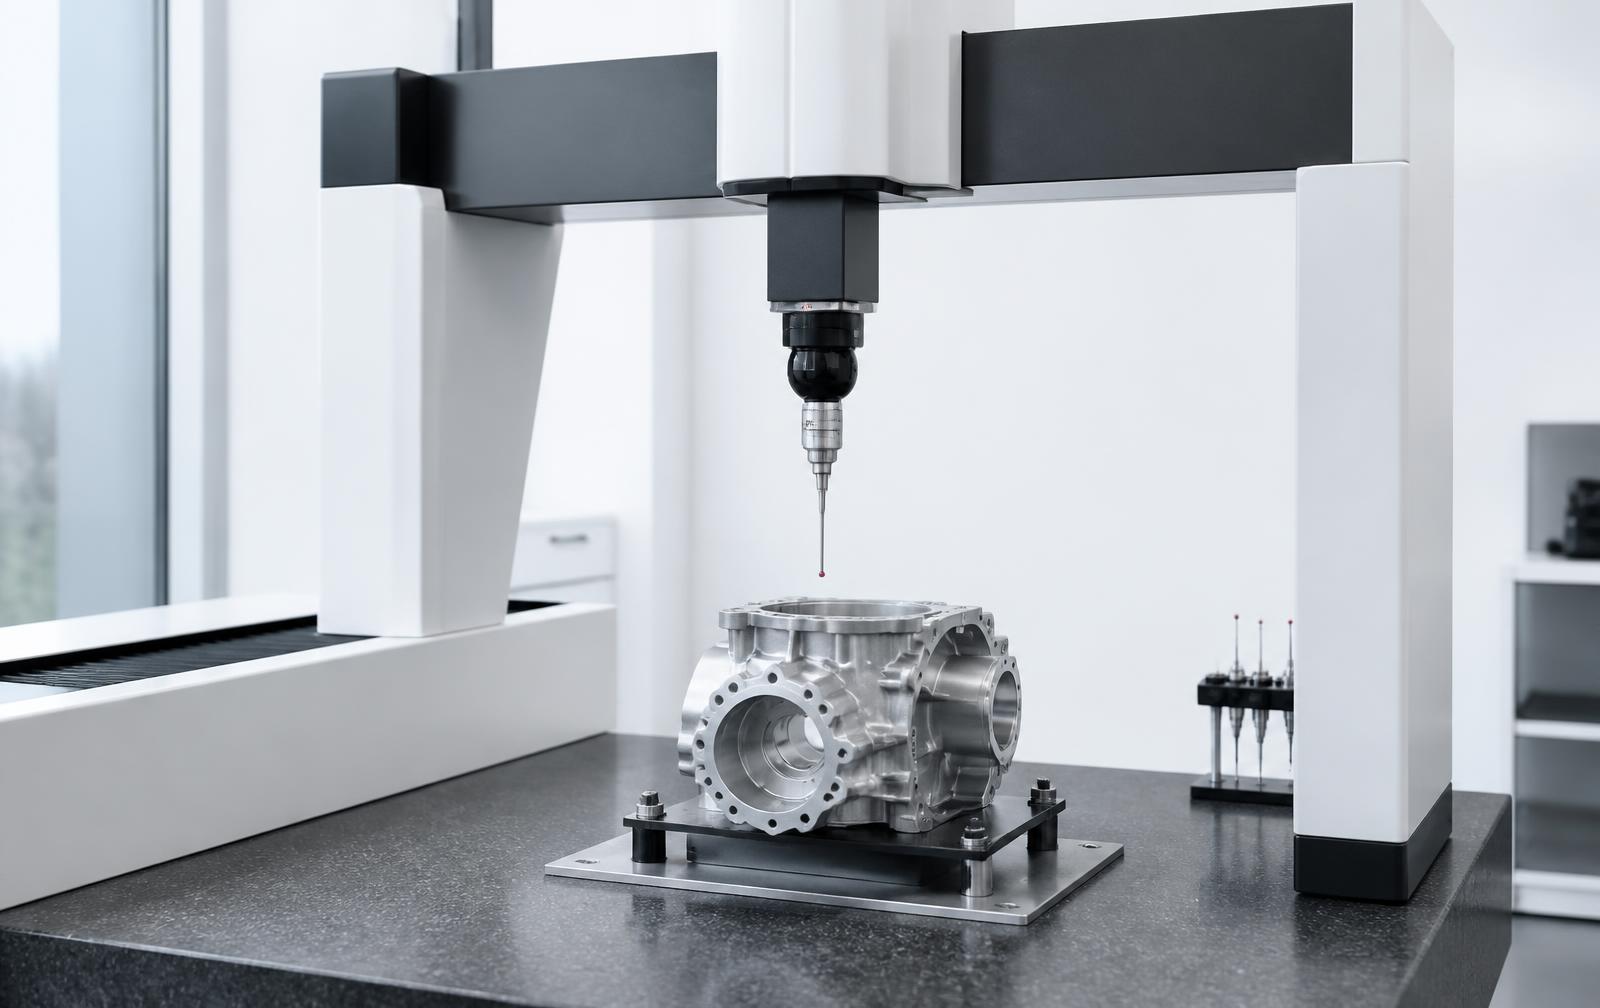
Tolerances are the part of a drawing that quietly sets the price. Two prints can describe the same geometry, in the same alloy, at the same quantity, and quote differently by a wide margin — because one of them specifies tight limits everywhere and the other reserves them for the features that actually control function.
This is not an argument for loose drawings. It is an argument for deliberate ones. Below is how tolerance decisions propagate into setup, tooling, inspection, scrap risk, and schedule, and how to structure a print so the cost lands where the engineering requirement is.
General tolerances vs. critical feature tolerances
Most drawings carry a title-block default — a general tolerance applied to any dimension without its own callout. Everything else is a specific callout: a tighter limit, a geometric control, a surface texture requirement, or a note.
General tolerances
These cover clearance holes, edge breaks, overall envelope dimensions, cosmetic radii, and features whose exact size does not affect assembly or function. They should be set at whatever the part can genuinely tolerate. A general tolerance is applied to dozens of dimensions at once, so tightening it is the single most expensive edit available on a drawing.
Critical feature tolerances
These are the features that determine whether the part works: bearing bores, sealing faces, press fits, mating interfaces, datum relationships, and anything a downstream assembly indexes from. Tight limits here are justified and expected. Calling them out explicitly also tells the machinist and the inspector where attention belongs.
The practical goal is a drawing where a reader can identify the critical features in a few seconds. When every dimension is tight, nothing is prioritized — and the process has to treat all of it as critical.
Where the cost actually accumulates
| Cost driver | Effect of unnecessarily tight limits |
|---|---|
| Setup | More careful indicating and datum pickup; fewer features can be combined into a single roughing pass; may force an extra setup to machine a feature in its most stable orientation. |
| Machining strategy | Roughing and finishing must be separated; lighter finish passes, reduced depth of cut, and additional spring passes to control deflection. |
| Tooling | Tools are replaced on wear-driven schedules rather than run to end of life, because dimensional drift matters sooner; some features require dedicated or ground-to-size tooling. |
| In-process control | More frequent operator checks between pieces, which adds non-cutting time to every part in the run. |
| Final inspection | More dimensions to measure, often on a CMM rather than with hand gauges, and longer measurement routines per part. |
| Scrap and rework risk | A narrower window means a smaller excursion turns a part into scrap; the quoted price has to absorb that risk. |
| Lead time | Every item above consumes schedule — proveout, slower cycles, longer inspection, and buffer for replacement parts. |
Why lead time moves, not just price
Cost and schedule are not independent. Tight work lengthens the calendar through several separate mechanisms:
- Longer proveout. First pieces are cut conservatively and measured before the program is released to run, so the front of the job takes longer.
- Slower cycles. Finish passes at reduced load add time to every piece, which compounds across a production quantity.
- Inspection queueing. Metrology is a shared resource. Parts requiring extensive CMM routines wait for machine time, and a full first-article package takes longer to produce than a dimensional spot-check.
- Recovery cycles. If a feature falls outside a narrow band, replacement parts re-enter the queue behind whatever is already scheduled.
This is why a drawing revision late in the process can be more expensive than the same change made before quoting: the process, tooling, and inspection plan were all built around the earlier callouts.
Practical steps that reduce cost without reducing function
- Set the title-block default to what the part genuinely needs, then tighten only specific features.
- Use geometric controls to describe the relationship that matters, instead of tightening several linear dimensions to imply it.
- Choose a datum scheme that matches how the part is located in assembly and how it can be held in a fixture.
- State whether a limit is functional or inherited from a legacy print — inherited callouts are often the easiest to relax.
- Specify surface finish only where it is required; a blanket fine-finish note affects the entire part.
- Identify which features need documented inspection results and which do not.
- Ask for feedback before release. A short review often finds one or two callouts carrying a disproportionate share of the cost.
Make the inspection plan part of the conversation
A tolerance is only meaningful alongside the method used to verify it. Measurement approach, datum setup, and fixturing all influence the reported result, so agreeing on how a feature will be measured avoids disagreements later about whether a part conforms.
Our approach to measurement and documentation is described under inspection and across the quality section, and the callout conventions we work to are on the tolerance standards page. If you would like a specific print reviewed for cost and schedule impact, send it with your request for quote and note which features are functionally critical.